
Vacuum diffusion bonding equipment

Diffusion Bonding Furnaces for Vacuum Solid-State Joining

Diffusion bonding furnaces from Haoyue for heat exchangers, titanium and dissimilar metals. DB series work zones 200×200×300 to 1000×600×1000 mm, vacuum ≤6.7×10⁻⁴ Pa.

Prefer direct contact?sales@haoyue-group.com+86-18917126064

Response timing confirmed after scope review

Material and process window reviewed first

Configuration proposal before model selection

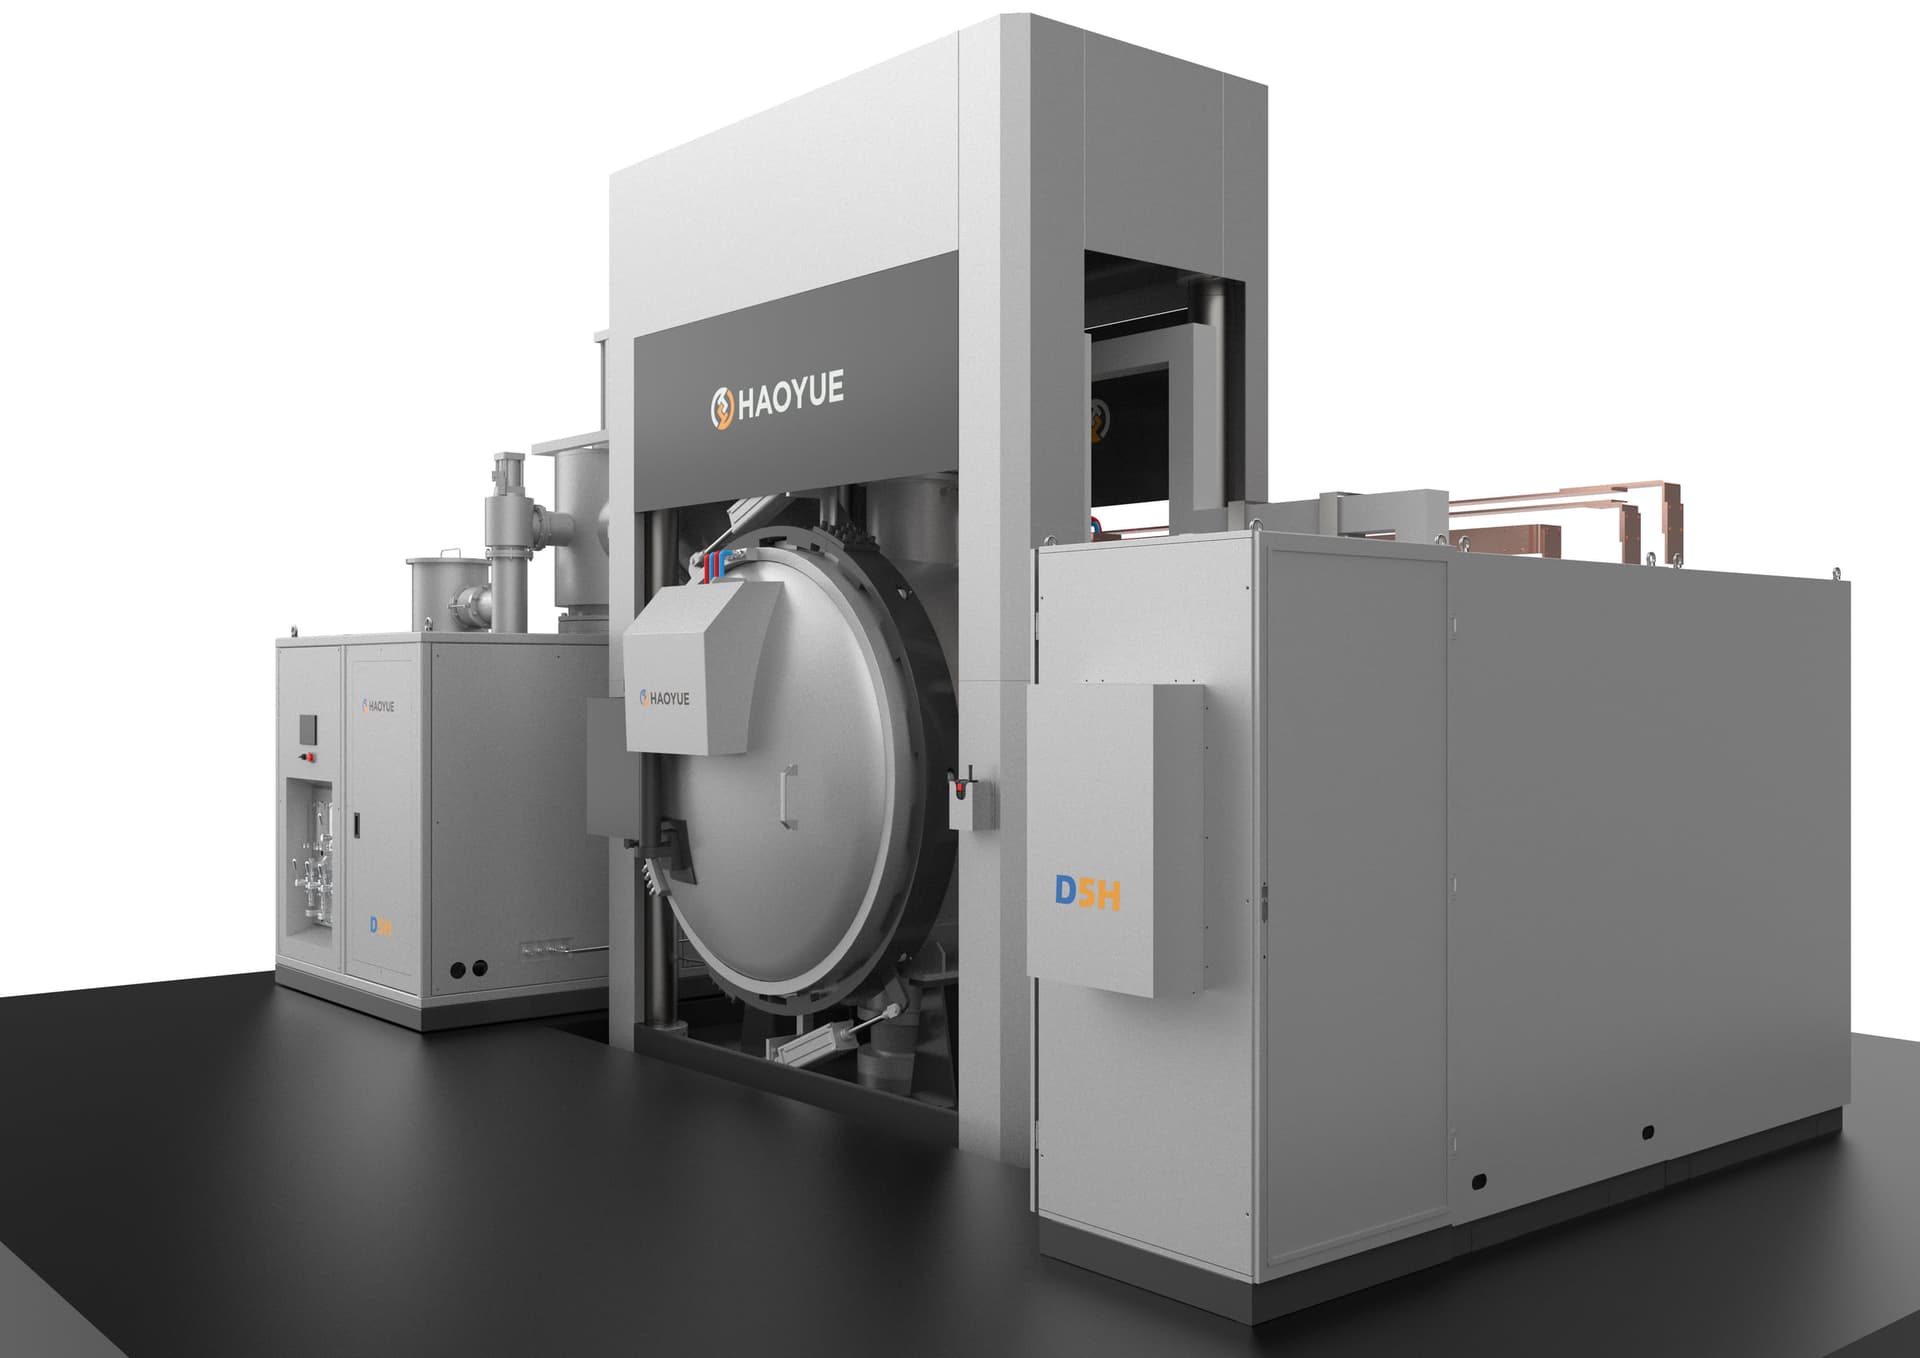
D Series vacuum diffusion bonding furnace

Start with the process window

Turn a keyword search into an engineering brief.

Haoyue designs and manufactures vacuum diffusion bonding furnaces for solid-state joining of metals, titanium assemblies, plate and microchannel heat exchangers, and other precision stacks. Equipment configuration begins with the material pair, channel or joint geometry, surface preparation, load path, temperature-pressure cycle, vacuum package, tooling interface, chamber size, inspection method, and project acceptance plan. Published equipment references do not replace material-specific bonding trials or joint validation.

Selection factors

Joint, channel, and material pair

Document the material pair, surface finish, coating or interlayer, joint and channel geometry, stack height, thickness, and thermal expansion considerations.

Load path and tooling

Define compressive load, flatness, fixture stiffness, alignment, stroke, and how the load reaches the complete bonded stack.

Vacuum and atmosphere

Confirm vacuum level, leak-rate expectations, purge gas, contamination limits, and whether a protective atmosphere is needed during cooling.

Inspection and records

Agree on dimensional checks, leak checks, bond inspection, witness samples, data logging, and acceptance documentation before quotation.

Bondable materials

Which materials can a diffusion bonding furnace join?

Diffusion bonding is a solid-state joining method: prepared mating surfaces are pressed together under heat in vacuum so atoms diffuse across the interface without a melted joint. It is particularly suited to materials that are difficult to join by fusion welding. Suitability is always confirmed for the specific material pair, surface route, and joint design.

Titanium and titanium alloys

Titanium assemblies are a common diffusion bonding route. Grade, surface preparation, cycle, and joint validation are defined in the project plan.

Titanium diffusion bonding process ->

Dissimilar metal combinations

Solid-state joining can connect dissimilar metals that are difficult to weld by fusion methods, subject to thermal-expansion and interface review.

Heat-resistant alloys

Heat-resistant alloys used in demanding thermal assemblies can be reviewed against the furnace temperature, load, and vacuum window.

Ceramics and intermetallic compounds

Ceramics and intermetallic compounds are listed among the materials suited to diffusion welding, including ceramic-to-metal joint concepts.

Composite materials and new materials

Composite and other new materials can be reviewed where a joint without filler metal or a melted zone is required.

Laminated metal stacks

Multi-layer plate and laminated stacks are bonded as one assembly, so tooling, flatness, and load distribution are reviewed with the furnace.

Heat exchanger stack guide ->

Published specifications

Diffusion Bonding Furnaces specifications

Model data below is taken from Haoyue's published product pages. Final values, process suitability, and acceptance criteria are confirmed for each quoted configuration.

DB series vacuum diffusion bonding furnaces

Published on the Vacuum Diffusion Bonding Furnace product page. Common values (maximum temperature, uniformity, vacuum, pressure rise rate, indenter parallelism, pressure and displacement accuracy, cooling gas pressure) are listed once for the series.

ModelEffective workspace (mm)Pressure tonnageNumber of indenters
DB-223200×200×30030~300Single / double
DB-446400×400×60030~300Single / double
DB-556500×500×60050~500Single / double
DB-666600×600×60050~500Single / double
DB-767700×600×700200~1000Single / double / quadruple
DB-868800×600×800200~1000Single / double / quadruple
DB-969900×600×900200~1000Single / double / quadruple
DB-106101000×600×1000200~1000Single / double / quadruple

DB series common parameters

Series-level values as published; final values are confirmed for the quoted configuration.

ParameterPublished value
Maximum temperature1300°C
Temperature uniformity≤±5°C
Ultimate vacuum≤6.7×10⁻⁴ Pa
Pressure rise rate≤0.5 Pa/h
Parallelism of upper and lower indenters≤0.1 mm
Pressure accuracy≤±0.5%
Displacement accuracyH±0.05 mm
Air cooling pressure2~10 bar

D series diffusion welding furnaces (D2 laboratory and D5/D8/D10 production)

Published on the D2 and D5H model pages.

ModelOperating temperature (°C)Chamber size (mm)Pressure (kN)Ultimate vacuum (Pa)
D2MO141400W200×H200×D300—6.7×10⁻⁴
D2GR202000W200×H200×D300—6.7×10⁻⁴
D5MO141400500×500×60020006.7×10⁻⁴
D8MO141400800×600×80050006.7×10⁻⁴
D10MO1414001000×600×100080006.7×10⁻⁴
Open the D5H model page ->

Applications

Diffusion bonding furnace applications

Haoyue diffusion bonding furnaces are configured for heat exchange assemblies, precision joining, laminated metal stacks, and aerospace structures. Each application changes the tooling, load path, and inspection plan.

Plate and microchannel heat exchangers

Plate count, channel pattern, perimeter seal area, and stack height drive the work zone, tooling stiffness, and leak-test plan.

Diffusion bonding heat exchangers ->

Titanium assemblies

Titanium projects separate furnace configuration from surface preparation, bonding-cycle development, and joint validation.

Titanium process inputs ->

Aerospace structures

Aerospace and gas-turbine assemblies need documented thermal, load, and vacuum records alongside the agreed inspection route.

Aerospace applications ->

Technical configuration reference

Scope the equipment around the process, not a generic model label.

These are configuration checkpoints for a technical proposal. Final values, process suitability, and acceptance criteria are confirmed for each project.

ParameterConfiguration referenceConfirm in the inquiry
Joint stack and materialsThe furnace and tooling review begins with the material pair, joint geometry, surface condition, and any interlayer or coating.Material pair, drawing, joint area, thickness, surface finish, and preparation route.
Heat-exchanger and channel stackPlate count, channel pattern, perimeter seal area, stack height, unsupported spans, and internal flow paths affect tooling stiffness and load distribution.Plate and channel drawings, complete stack height, bonding area, flatness targets, and protected flow passages.
Temperature and thermal fieldHeating zone, temperature range, measurement points, dwell sequence, and controlled cooling are matched to the bonding cycle.Bonding temperature, dwell, ramp profile, temperature tolerance, and cooling limit.
Load path and toolingPress capacity, stroke, platen or ram arrangement, fixture stiffness, and alignment are reviewed around the complete bonded assembly.Required pressure or load, stroke, fixture drawing, flatness, and full stack height.
Vacuum and atmosphereVacuum package, purge gas, cleanliness controls, and cooling atmosphere are selected for the material pair and joint protection needs.Vacuum target, gas type and purity, leak-rate expectation, and contamination limits.
Validation and recordsData logging, witness-sample handling, safety functions, and documentation are set around the agreed inspection and acceptance plan.Inspection method, record requirements, witness samples, acceptance criteria, and delivery region.

Supplier comparison evidence

Ask for evidence that can be checked during acceptance.

A catalogue limit does not prove project fit. Use the same written evidence request when comparing manufacturers, then carry the agreed checks into factory and site acceptance.

Load distribution and tooling basis

Review in the proposal

Compare the proposed press capacity, platen arrangement, fixture stiffness, alignment method, and complete joint-stack envelope against the actual bonding area.

Confirm for acceptance

Agree on tooling drawings, load and position records, alignment checks, and the witness or dummy stack used during factory review.

Thermal and vacuum records

Review in the proposal

Confirm where temperature, vacuum, pressure, and cooling data are measured and how those measurements represent the bonded stack.

Confirm for acceptance

Define the recorded channels, sensor checks, empty-furnace or loaded verification conditions, leak-rate method, and report format before order release.

Joint inspection route

Review in the proposal

Separate furnace capability from material-specific joint validation by defining dimensional, leak, metallographic, mechanical, or nondestructive checks for the project.

Confirm for acceptance

Assign responsibility for samples, inspection methods, acceptance limits, retained records, and any third-party test requirements.

Factory and site handover

Review in the proposal

Compare suppliers using one written scope for utilities, safety interfaces, documentation, training, installation, commissioning, and site acceptance.

Confirm for acceptance

List the factory acceptance test, open items, delivery documents, site prerequisites, training scope, and final sign-off responsibilities.

Review path

Four checks before a configuration is selected.

01

Describe the joint stack, surface preparation, bonding area, and target interface condition.

02

Define temperature, load, dwell, atmosphere, vacuum, and controlled cooling requirements.

03

Review fixture stiffness, alignment, usable chamber, heating uniformity, and measurement method.

04

Set inspection, witness-sample, documentation, and acceptance requirements.

Frequently asked questions

What is a diffusion bonding furnace?

A diffusion bonding furnace is a vacuum furnace with a pressing system that joins prepared mating surfaces through atomic diffusion under heat and sustained pressure, without a melted interface. The bonding temperature is typically 50-90% of the base material's melting temperature, and parts are cooled under vacuum before unloading.

Which diffusion bonding furnace sizes does Haoyue offer?

The published DB series ranges from DB-223 with a 200×200×300 mm effective workspace to DB-10610 with 1000×600×1000 mm, with single, double, or quadruple indenters depending on the model. The D2 laboratory furnace has a W200×H200×D300 mm chamber, and the D5, D8, and D10 production models are listed with 2000, 5000, and 8000 kN pressure.

Which materials can be diffusion bonded?

Diffusion bonding is particularly suitable for dissimilar metals, heat-resistant alloys, titanium, ceramics, intermetallic compounds, composite materials, and other materials that are difficult to join by fusion welding. The specific material pair and surface route must be validated for each project.

What information is needed for a vacuum diffusion bonding furnace quotation?

Send the material pair, joint drawing, bonding area, surface condition, temperature, pressure, dwell, vacuum, fixture, chamber envelope, and acceptance requirements. Available process data and inspection plans help us prepare a more accurate technical proposal.

Can Haoyue configure a furnace for titanium, heat exchangers, or precision assemblies?

Yes. Furnace temperature, pressure system, vacuum package, chamber size, tooling interface, cooling, control records, and safety functions are configured against the material pair, joint geometry, load path, and validation plan.

What should a heat-exchanger project define before furnace selection?

Provide plate and channel drawings, material grade, complete stack height, bonding area, surface preparation, target temperature and pressure cycle, fixture concept, dimensional limits, leak-test plan, and the inspection route used to accept the bonded assembly.

Does a furnace specification validate a titanium diffusion bonding process?

No. The equipment specification defines available temperature, load, vacuum, tooling, controls, and records. Titanium surface preparation, bonding parameters, microstructure, joint properties, and inspection acceptance remain part of the material and process validation plan.

Is diffusion bonding the same as brazing?

No. Diffusion bonding relies on prepared surfaces, heat, pressure, and time to form a solid-state joint; brazing uses a filler metal. The correct route depends on material compatibility, joint design, temperature limits, and inspection needs.

What determines the press size?

The press is reviewed against bonding area, required pressure, fixture stiffness, stroke, alignment, and the complete assembly envelope, not only the material name.

What should be validated before a production order?

Validate the thermal and load records, bond inspection method, dimensional limits, witness-sample plan, safety functions, and documentation package.
Next step

Share the process window for an engineering review.

Send the material or part, temperature, pressure, atmosphere, work zone, and project goal. Haoyue can review the equipment configuration and identify missing inputs. Process results remain subject to the agreed trial and acceptance criteria.

Use the Full Technical Form
WhatsApp